Intermittent Bonded Ribbon Production Line For Sale
With a listed operating speed of 600 m/min, this machinery offers substantial capacity for optical-fiber production. Before making purchasing plans, buyers should verify the actual speed, configuration, and operating conditions with the manufacturer.
Shanghai Weiye OFC supplies equipment designed specifically for producing rollable ribbons containing 12 or 16 fibers. The published product information covers capabilities, technical details, and supplied systems, helping U.S. buyers begin evaluating the equipment against their manufacturing needs.
Begin by examining the stated equipment configuration, then ask the supplier for pricing, installation requirements, and project-specific alternatives. This approach helps determine which equipment details apply to your particular manufacturing site and goals.
The listed address for Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. is 201 Minyi Road, Songjiang District, Shanghai. Use the product page for initial reference and verify current technical and commercial information directly with the company. Submitting a clear request for pricing and specifications can help you move forward with the assessment.
Intermittent Bonded Ribbon
Fiber Coloring Machine
SZ Stranding Line
Important Points To Consider
- The stated operating speed is 600 m/min, although the manufacturer should confirm the applicable conditions.
- This equipment supports production of 12-fiber and 16-fiber rollable ribbon formats.
- The product listing describes machine capabilities, technical specifications, and supplied systems.
- Request details about pricing, installation requirements, and project-specific customization.
- A company address in Shanghai’s Songjiang District is included in the supplier information.
Overview Of The Intermittent Bonded Ribbon Production Line
According to the supplier, the equipment is designed for rollable IBR configurations containing 12 or 16 fibers. Its product page specifies a construction speed of 600 m/min and a fiber diameter of Ф245 μm ±10 μm. As these are manufacturer-listed values, confirm the actual production speed and relevant operating requirements directly with the supplier.
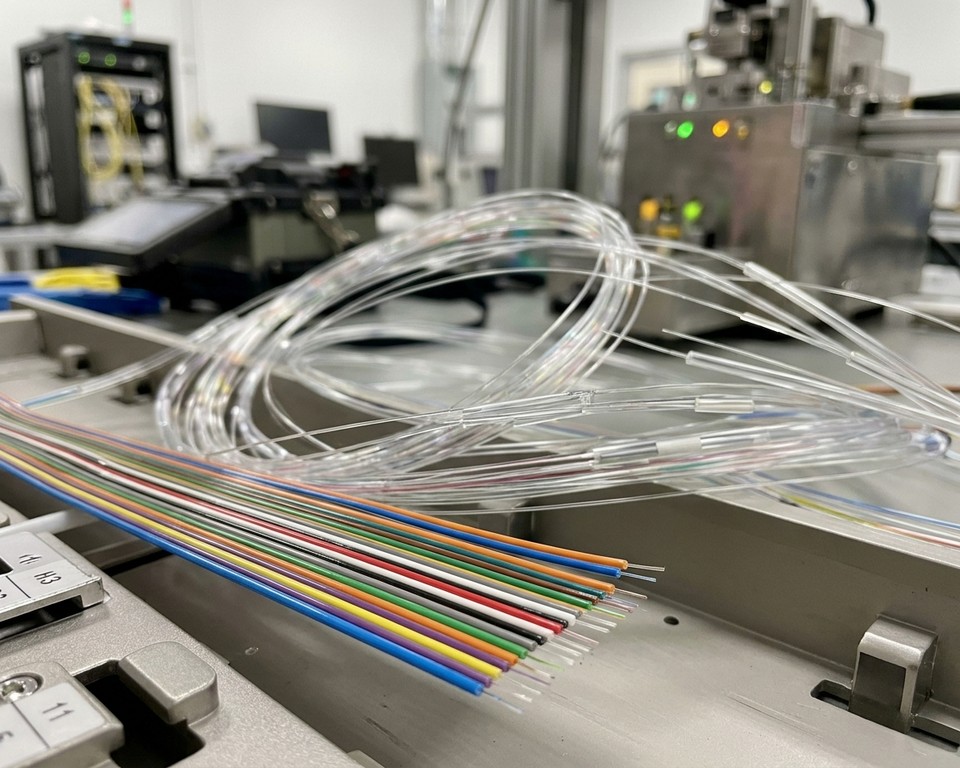 Intermittent Bonded Ribbon Production Line
Equipment Designed For Twelve- And Sixteen-Fiber Rollable Ribbon Production
The machine configuration accommodates two different fiber counts in rollable ribbon designs. Buyers can use these options as a starting point for checking compatibility with target formats, fiber sizes, and handling requirements.
How Intermittent Bonding Supports Flexible Fiber Arrangement
The patent’s design examples describe neighboring fiber subunits joined by adhesive bonds positioned at intervals. The patent provides an example of adhesive-bond intervals ranging between 10 mm and 1,000 mm. This differs from a continuously bonded structure in which the connection extends across the full ribbon length.
By spacing the bonds apart, the assembly can move between a mostly planar arrangement and a rolled, curled, or folded shape. The specified spacing illustrates the patented design concept rather than confirmed production-machine settings.
- Machine details: A choice of 12 or 16 fibers, a listed operating speed of 600 m/min, and a specified diameter of Ф245 μm ±10 μm.
- Patent example: Illustrative spacing between adhesive bonds of 10 mm to 1,000 mm.
- Design benefit: Adaptable handling when the ribbon takes different shapes.
Applications In Optical Fiber Cable Manufacturing
Flexible ribbon arrangements can help cable designers balance access for splicing with compact cable packaging. The patented design keeps fibers arranged in order while permitting sections between bonded points to shift as the cable is assembled.
Compact Cable Designs And High Fiber Density
An optical fiber ribbon may remain flat during mass fusion splicing and subsequently fold or roll for installation in a smaller cable. The patent identifies opportunities for reduced cable dimensions and a greater proportion of fiber area relative to the cable’s cross-sectional area. Actual performance and dimensions will vary according to the overall cable design and the application for which it is intended.
Ribbon Organization For Efficient Fusion Splicing
This design supports orderly fiber handling during splicing while providing flexibility for subunit movement in the assembly process. The manufacturer’s material-handling specifications identify payoff reel capacities of 25.2 km and 50.4 km of fiber. These reel capacities can be compared with the facility’s cable-manufacturing needs and material-handling setup.
| Design detail | Possible application | Buyer consideration |
|---|---|---|
| Flat fiber configuration | Fusion splicing of multiple fibers | Confirm requirements for the splice workflow |
| Folded or rolled format | Space-efficient cable packaging | Examine the complete cable design |
| Payoff reels with capacities of 25.2 km and 50.4 km | Planning material-handling operations | Match the reel capacity to production operations |
Specifications And Performance Of The Production Line
Compare the equipment’s published performance figures with your manufacturing requirements before requesting a quotation. Installation preparations should also account for suitable reels and the utilities available at the production site.
Speed, Diameter, And Attenuation
The stated construction speed is 600 m/min. The listed fiber diameter is Ф245 μm ±10 μm, with additional attenuation of ≤0.01 dB/km measured at 1550 nm. Confirm the measurement conditions and expected performance directly with the manufacturer.
Compatibility With Payoff And Take-Up Reels
The payoff system accommodates two reel dimensions, and the maximum weight of a full reel is 10 kg. The take-up assembly supports a T-type reel as well as a fiber-optic reel. Verify that your selected reel configuration is compatible with the facility’s material-handling process.
Site Utilities And Environment
The machine requires a three-phase, five-wire electrical supply rated at 380 V ±10%. The equipment should operate in an enclosed, clean, dry, draft-free area maintained at 15 to 25°C and a maximum relative humidity of 85%. Nitrogen must be supplied at 7 bar with 99.99% purity, together with compressed air at 6 bar. Verify the required utility connections before installation begins.
| Specification | Listed requirement | Installation planning note |
|---|---|---|
| Reels for fiber payoff | Payoff dimensions of Ф236 × Ф25.4 × 108 mm or Ф267 × Ф25.4 × 180 mm; full reel ≤10 kg | Verify reel dimensions and weight |
| Take-up reel | T-type dimensions of Φ410 × Φ50.8 × 391 mm, or a fiber-optic reel | Verify the preferred reel format |
| Power and environment | 380 V ±10%; 15 to 25°C; relative humidity ≤85% | Prepare a dry, clean, draft-free operating area |
| Gas utility supply | Nitrogen: 7 bar, 99.99% purity; air: 6 bar | Verify gas supply capacity before installation |
Fiber Payoff And Gathering Equipment
Optical fibers are guided toward the forming section by the payoff and gathering components. Their control systems support consistent feeding and help protect individual fibers throughout handling.
Tension-Controlled Payoff System For Sixteen Spools
The payoff assembly holds 16 spools and provides traversing along with separately adjustable tension settings. The permitted weight for an individual spool is up to 10 kg. Detailed specifications indicate a tension range of 0.4 to 2 N, accuracy of ±0.02 N, and a 550 W motor. Another overview gives a range of 40 to 150 g and accuracy of ±2 g, so buyers should confirm which specification applies to their configuration.
Fiber Guiding, Break Detection, And Electrostatic Control
The forming area receives fibers through U-groove guides, multi-groove gathering rollers, and devices designed to prevent jumping. Operators receive alerts about fiber problems through break detection and alarm functions. Protective guards and pneumatic clamping provide additional support for safe material handling. At the fiber exit, a rod-style electrostatic dust collector is installed, while anti-static equipment helps manage dust along the gathering route.
| Equipment component | Listed detail | Purpose |
|---|---|---|
| Payoff | 16 spools with a maximum of 10 kg each | Supplies fibers using traversing |
| Tension and motor | Tension of 0.4 to 2 N, accuracy ±0.02 N; motor rated 550 W | Supports regulated payoff of fibers |
| Fiber guidance and safety features | Rollers with grooves, warning alarms, protective guards, and a pneumatic clamp | Directs fibers and supports safe handling |
| Electrostatic management | Rod-type dust collector and anti-static equipment | Supports dust control along the fiber path |
Intermittent Adhesive Dispensing And Precision Molding
The ribbon-forming platform allows operators to control the mold position and placement of adhesive. These settings allow the production process to be adapted to the intended ribbon configuration.
Ribbon Formation Using An Adjustable IBR Mold Platform
Ribbon formation uses three mold assemblies, each capable of holding up to five Nordson EFD jet valves. Operators can position the mold within 0 to 15 mm and adjust its base temperature from 20°C to 60°C. Precision valve groups mounted on sliding tables allow fine positioning and accurate application of adhesive dots.
Adjustable Nozzle Configurations For Twelve- And Sixteen-Fiber Ribbon Production
The 12-fiber configuration employs a 5+5+1 valve arrangement. The 16-fiber format is produced using a 5+5+5 valve layout. The control interface enables changes to dot count and spacing according to the ribbon configuration being manufactured. The process calls for a specialized adhesive suitable for both coating and curing.
| Setting | 12-Fiber Format | Format With 16 Fibers |
|---|---|---|
| Valve arrangement | Valve arrangement of 5+5+1 | 5+5+5 valve configuration |
| Mold positioning range | 0 to 15 mm adjustment | Adjustment range of 0 to 15 mm |
| Mold-base temperature | Temperature range of 20°C to 60°C | Temperature range of 20°C to 60°C |
UV-LED Curing For Bonded Fiber Ribbons
Adhesive across the fiber assembly is cured through a sequence of UV exposure stages. The arrangement of the ovens and their published operating values provide buyers with information for evaluating process compatibility.
Pre-Curing And Main Curing Stages
Pre-curing is handled by three specialized 800 W LED-UV ovens. Each oven processes fibers supplied by a separate mold group before the material reaches the main 6 kW post-curing oven. Adjustable shutters reduce potential UV leakage and nitrogen loss. The supplier states a principal wavelength of 395 nm ±3 nm, minimum curing degree of 85%, and post-curing power of no less than 2.5 kW.
Nitrogen Management And Curing Performance
The nitrogen flow rate and pressure can be adjusted by hand. Automatic functions also start nitrogen delivery during startup and stop it at shutdown. The manufacturer states that lamp-array power use remains at or below 80% of total power during steady, continuous operation at production speed. These specifications provide a reference for comparing equipment, although testing conditions should be verified with the supplier. Ask whether different adhesives or materials require adjustments to the settings.
Visual Inspection, Capstan Traction, And Take-Up
Visual inspection and consistent winding help preserve fiber quality as material passes through the production line. The published operating settings also offer buyers useful criteria for comparing equipment against their cable production requirements.
Real-Time Inspection Of Fiber Colors And Adhesive Dot Placement
Real-time magnified views are displayed through the machine’s microscope and camera system. Operators can inspect optical-fiber color order and verify the presence of resin dots at individual dispensing locations. By examining the optical fiber ribbon during production, operators can detect potential issues ahead of winding.
Servo-Driven Traction And Precision Take-Up
The Φ190 mm capstan traction wheel is driven by a 1 kW AC servo motor. The listed measurement accuracy exceeds 1‰. Operators can set tension between 50 and 500 g while maintaining an accuracy of ±5 g. These operating parameters help maintain careful fiber-ribbon handling as the material advances through the line.
The specified take-up speed is 600 m/min, and the maximum spool weight is 30 kg. The servo-driven take-up and traversing assemblies support uniform positioning during winding. Cable pitch can be adjusted continuously between 1 and 6 mm. Position detection and direction changes are supported by a photoelectric sensor. Confirm that the operating conditions and settings are suitable for your target cable design with the supplier.
Production Monitoring And Electrical Control Systems
Accessible controls allow operators to adjust settings, check equipment status, and arrange orderly shutdowns. According to the manufacturer, the machinery incorporates Siemens controls alongside Schneider Electric switchgear.
Operating The Production Line Through PLC And Touchscreen Controls
The ribbon production line uses Siemens S7-1200 and S7-1500 PLCs with a 10.4-inch Siemens touchscreen interface. Low-voltage switchgear is supplied by Schneider Electric. The system supports both interlocked operation across the full production line and separate operation of individual units.
Process Settings, Warning Alarms, And Preset-Length Shutdowns
Through the touchscreen, operators can manage process settings, activate curing ovens, configure wire feeding, and view alarms. Additional displays provide lamp runtime, real-time current readings, curing-oven temperature, and total machine operating hours. A meter-counter correction function helps synchronize displayed length measurements with actual material movement.
A preset length can be entered to initiate slowing or stopping of the machine. The function supports managed stopping as a cable manufacturing run reaches its planned length. Verify the available controls and configuration requirements with the supplier before purchasing.
| Control feature | Listed detail | Use |
|---|---|---|
| PLC and display | Siemens S7-1200/S7-1500; 10.4-inch touchscreen | Configure settings and examine production data |
| Electrical control components | Schneider Electric low-voltage switchgear | Supports electrical control operations |
| Equipment monitoring and shutdown control | Lamp, oven, runtime, and meter information with preset length | Monitor production and stop or decelerate the equipment |
Materials, Process Compatibility, And Ribbon Quality
Adhesive selection affects both the consistency of coating application and the final product. Rather than recommending a general adhesive, the supplier specifies a formulation dedicated to the equipment’s coating and curing operations.
Dedicated Adhesive For Bonding And Curing
The pressure-fed adhesive system provides independent valve switches so each supply path can be opened or closed as required. Adhesive flow to each dispensing point is managed using precision pressure-control valves. The specified air pressure is adjustable, with a required minimum of 0.5 MPa.
Black adhesive supply tubing helps protect the material from reactions caused by UV exposure during operation and curing. Preventing unintended exposure matters because adhesive behavior could be affected before the material reaches the fiber surface.
Before selecting materials for a secondary coating line, verify adhesive compatibility, production settings, and required surface-quality standards with the supplier. Discuss the material’s expected performance across your planned application and run duration. Clear process instructions can help maintain quality from initial setup through final production.
Installation Requirements And Included Documentation
Prepare the installation area and necessary utility connections before arranging equipment setup. The manufacturer’s stated requirements help buyers prepare their facilities and maintain stable operation of the optical fiber equipment.
Facility Conditions And Buyer-Supplied Connections
The machine should be positioned inside a draft-free, enclosed workspace that is clean and dry. Keep the operating area between 15 and 25°C, with humidity at or below 85%. The installation also requires nitrogen supplied at 7 bar with 99.99% purity and an air supply rated at 6 bar.
The equipment package does not include connecting cables or cable trays. The purchaser is responsible for supplying the main incoming power cable. Verify the available utilities and planned cable routes ahead of setup, especially if a secondary coating section is nearby.
Operating Manuals, Drawings, And Maintenance Information
Documents covering installation, equipment use, and maintenance are provided by the manufacturer. Inspect the supplied documentation before commissioning so personnel can organize tasks and obtain required materials.
- Operating and instruction manuals together with the overall equipment layout drawing
- Electrical schematics, wiring diagrams, and drawings for installation and maintenance
- Purchased-component instructions and a wear-parts list to support service preparation
The supplied records support preparation for commissioning and routine servicing of the cable production machinery.
Selecting A Ribbon Production Line That Matches Your Manufacturing Requirements
First determine which finished ribbon products your business plans to offer. This production line is designed for 12F and 16F options, with a listed construction rate of 600 m/min. Compare those specifications with your expected product mix, production targets, and anticipated cable demand.
Verify take-up reel compatibility before placing an equipment order. A standard IBR reel measures Φ410 × Φ50.8 × 390 × Φ310 mm, accommodates a maximum weight of 30 kg, and allows cable pitch settings between 1 and 6 mm. Check that these specifications suit your production facility and material-handling operations.
The compatibility of payoff spools should be reviewed as well. Available options include international-standard spools accommodating 25.2 km, 50.4 km, and 63 km. Obtain the exact spool dimensions before ordering materials or planning the length of manufacturing runs.
Evaluate utilities, adhesive requirements, and operator-monitoring capabilities alongside production speed. Assess whether the equipment arrangement is appropriate for fiber cable, loose tube, or the specific application in your cable production process. Before ordering, review equipment configuration and startup requirements directly with Shanghai Weiye. Checking equipment suitability in advance can reduce the likelihood of costly changes after purchase.
| Planning point | Listed detail | Buyer check |
|---|---|---|
| Ribbon configurations and operating speed | 12F and 16F formats; 600 m/min | Match the specifications to manufacturing goals and product range |
| Take-up configuration | 30 kg maximum capacity; adjustable pitch from 1 to 6 mm | Verify that the reel and site arrangements are suitable |
| Fiber payoff reel options | 25.2 km, 50.4 km, and 63 km spool capacities | Confirm the precise reel measurements |
How To Request A Quotation For The Intermittent Bonded Ribbon Production Line
U.S. buyers can evaluate a system offering 12F and 16F formats, a specified construction rate of 600 m/min, and specialized optical fiber ribbon-forming equipment. Compare these features with your planned cable products to assess equipment suitability.
When requesting a quotation, provide the required ribbon format, expected output volume, preferred reels, and available site utilities. Include information about the fibers and material-handling process to allow Shanghai Weiye to review the intended setup.
Confirm the suitability of the adhesive, the LED wavelength specification of 395 nm ±3 nm, and expected curing results before purchasing. Discuss how the stated specifications affect your intended material and finished surface-quality objectives.
Use the manufacturer’s product listing to examine the equipment information. Contact Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. to confirm machine configuration, delivery arrangements, and commissioning requirements. The supplier provides its address as 201 Minyi Road, Songjiang District, Shanghai. Telephone 021-60701630 to discuss your manufacturing requirements. Providing complete information in your quote request makes the following stages easier to clarify.